
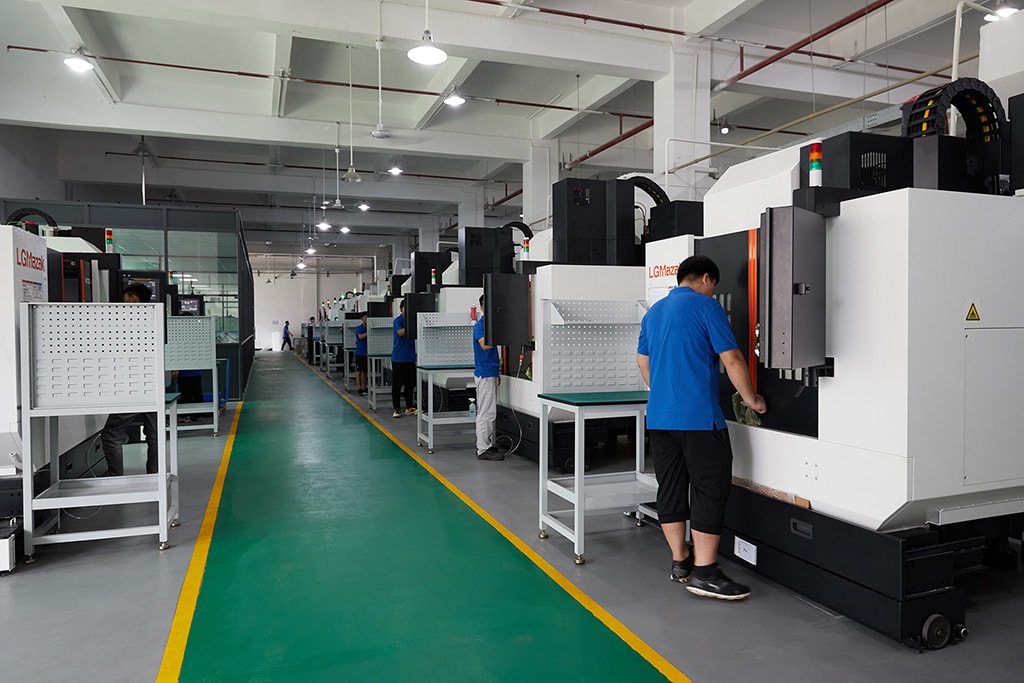
Custom machined parts are bought on their drawings, and the drawings are won or lost on their tolerances and finishes. But the numbers on a drawing do more than describe the part; they buy processes, measurement time, and risk. A blanket tolerance note prices every feature as critical whether it is or not, and a finish spread over the whole part pays for smoothness no function uses. The realistic discipline is different: assign each feature its own band, measure each from a named datum, call the finish where it functions, and let the RFQ carry the scheme so the numbers you specify are the numbers you receive. This guide explains that discipline, feature by feature.
What does a tolerance on a custom part actually commit the shop to?
A tolerance is a process selector disguised as a number. When the drawing says a bore is ±0.003 mm, the shop hears "controlled machining and a CMM check"; when it says the same bore is ±0.1 mm, the shop hears "standard cut and a gauge." The difference between the two is real money and real calendar, because every tightened feature adds a measurement step and a scrap risk to the route. A feature that drifts out of its band stops the lot; a feature that was never critical but carried a tight band is a feature that paid for precision it never needed.
The buyer's discipline is to read every tolerance as a purchase. Tighten only what the assembly needs, and leave the rest to a stated general class such as ISO 2768-m, which gives every open dimension a defined default without paying precision pricing. The drawing that names its general class and then tightens only the functional features is a drawing the shop can price honestly, because the price of a tolerance is only honest when the tolerance is real. The capability the shop holds is the same frame this site documents on its quality page, and it is the frame your drawing should speak to.
Why is a single blanket tolerance the wrong default?
A blanket note such as "all dimensions ±0.003 mm" is comfortable to write and expensive to make, because it converts clearance holes, cosmetic faces, and structural webs into critical characteristics. Every one of those features then carries precision machining and inspection time, and the part prices itself as if every surface sealed against something. The blanket note also hides the real tolerance story: with everything tight, nothing is prioritized, and the shop cannot see which features the assembly actually depends on.
Replace the blanket with a scheme. State the general class for the majority of dimensions, then list the specific features that carry function with their own bands — the bore that locates, the face that mates, the journal that spins. The scheme does not loosen the part; it directs the precision to where the part works. A drawing with ten tight features that matter and a general class for the rest is cheaper to make, faster to inspect, and easier to trust than a drawing where every feature is tight and nothing is prioritized.
Which features deserve the tight band on a custom part?
The tight band belongs on features that engage another part: a locating bore that positions an assembly, a bearing seat that carries a load, a mating face that establishes an interface, a journal diameter that fits a housing. These are the features where a relaxed tolerance changes the outcome — the assembly wobbles, the bearing runs hot, the part does not fit. Clearance holes, cosmetic faces, and structural webs carry no such consequence, and giving them precision spends budget and inspection time for no functional return.
Test every tight callout with one question: what fails if this feature relaxes to the next band? If nothing fails, the tolerance is decoration and the price is real. If the assembly fails, the tolerance is function and the expense is justified. The test converts tolerance assignment from habit into engineering, and it is the same test the shop's process engineers would run if they were setting the drawing. Buyers who run it before the RFQ find their parts cost less, inspect faster, and arrive more often on the date, because the features that actually matter got the attention they deserved.
Which datum and position scheme keeps the callouts consistent?
Tolerances mean nothing without a datum to measure from, because a feature measured from the wrong reference passes its report and fails its assembly. The drawing should name the surfaces that establish the reference frame — usually the primary mounting face and the two features that orient the part — and every positional callout should reference that frame. When a dimension is tightened, its datum should be tightened with it, because a precision band on a feature that floats from an uncontrolled datum is a precision band on paper only.
Where the design uses positional tolerancing, let the scheme carry the logic. Position tolerances with true-position callouts describe what the assembly needs — where the hole center must be relative to the datum — more honestly than coordinate dimensions that stack their errors. The buyer does not need to be a GD&T expert to ask one question: which surface is the reference for this feature, and how is it established at inspection? A supplier that answers with the datum and the inspection method is measuring the part the way the drawing intends; one that cannot is measuring the part the way the fixture happens to hold it.
What is the realistic precision ladder for a machined part?
The realistic ladder for custom machining is short and honest. Most dimensions should live on the general block, which covers fit-and-function without pulling in special processes. The controlled band — around ±0.003 mm on milled and turned features — is where locating and mating characteristics run, verified with CMM measurement. The precision band — around ±0.002 mm — belongs to grinding, a separate process family with its own machines and its own inspection. Below the general block sits ISO 2768-m as the default for open dimensions, and the ladder between general and controlled carries the intermediate bands that cover most real fits.
The ladder is read in both directions. Reading down shows what a feature costs as it tightens; reading up shows what a feature saves as it relaxes. Process capability sits on top of the ladder as the second test: a feature held at Ppk ≥ 1.67 initial across the run is a feature whose process is centered and stable, while a feature that relies on the luck of the first article is a gamble whatever the band says. The capability figure is what separates a drawing that is realistic from one that is merely tight, and it is the figure a buyer should request on every critical characteristic.
Which surface finish values belong in the drawing?
Surface finish is specified as Ra in micrometers, and the ladder tracks the process. As-machined surfaces typically land near Ra 3.2 µm, which falls out of a normal milling or turning pass and covers most general surfaces. Ra 1.6 µm needs fine machining and suits mating and seal-contact faces. Ra 0.8 µm means a grinding pass or a deliberately controlled finish cut, and it belongs on bearing seats, rotating journals, and sealing surfaces. Below that, Ra 0.4 µm and finer require grinding, lapping, or polishing, and they should be reserved for sliding and sealing applications where the function genuinely earns them.
Each step down the finish ladder adds an operation and a measurement, which makes finish a purely additive cost driver. The buyer's discipline is to call the finish where it functions and leave the rest on the as-machined default, so a sealing face at Ra 0.8 µm and the bracket beside it at Ra 3.2 µm share one drawing without sharing one process. The most common way a drawing raises its own price is to spread the fine finish across the whole part, and the fix is the same as for tolerances: specify the feature, not the blanket. When the finish is functional, ask how it is measured and how the edges and threads of that surface are finished, because the Ra on the face is not the whole story of the surface.
How do finishing treatments change what you measure?
Machining is rarely the last step, and every post-machining treatment changes the surface. Anodizing grows a coating layer that increases the dimension and changes the surface character; plating does the same in metal; passivation changes the chemistry without measurable thickness; and blasting or other mechanical finishes deliberately roughen what machining smoothed. A part machined to final size before anodizing can emerge oversized for its coating, and a sealing surface whose finish was specified on the base metal is not the same specification after the treatment covers it.
Specify the finished state and the path to it in one line: the machined tolerance with its allowance, the treatment, and the finish that counts after the treatment. State whether the critical Ra applies to the base metal or to the coated surface, because the two are different specifications and different measurements. Confirm that dimensions are verified when the part returns from the treatment, and that the report reflects the finished state rather than the pre-treatment state. A drawing that names the treatment, the allowance, and the post-treatment verification is a drawing whose finish survives the process; one that leaves the treatment unmentioned is a drawing whose expectations end at the machine door.
Which measurement evidence closes the loop on a callout?
A tolerance and its measurement belong in the same sentence. The report should name the instrument for each critical feature — a CMM for a bore and its position, a dedicated gauge for a thread, a roughness tester for a finish — and the result against the tolerance. Where the tolerance is narrow enough that measurement uncertainty matters, the report should acknowledge it. A number without a method is not evidence; it is an assertion, and assertions do not survive an audit or a failed assembly.
For critical characteristics, ask for the process behind the numbers, not just the values. Capability data drawn from across the run shows the process stayed centered; a single measured value shows only that one part passed at one moment. When the drawing carries features at ±0.003 mm by milling and turning, or ±0.002 mm by grinding with Ppk ≥ 1.67 initial-study targeted on criticals, the measurement plan should prove both the parts and the process. The report that carries part values and process evidence together is the report that closes the loop, and it is the report a buyer should require in the RFQ rather than hope for at delivery.
How do you write the RFQ so the numbers you specify are the ones received?
The RFQ is where the tolerance scheme becomes a contract, and it should carry the whole scheme rather than a note. State the general class for open dimensions, list the tight features with their bands and their datum references, name the finish per feature with its process expectation, and list the measurements the report must contain. Ask the supplier to confirm per feature what it will hold and how it will measure, so the quotation is for the part you drew rather than the part it assumed. The cost page for custom machining on this site, at how-much-does-custom-machined-part-cost-in-2026-a-buyer-s.html, shows how the tolerance scheme lands in the price, and the parts page at custom-machined-part-parts.html shows the finished features the scheme protects.
Then let the first article do the final check. When the sample arrives, compare the report against the scheme — feature by feature, instrument by instrument — and approve or reject against the drawing rather than against a feeling. A first article that confirms the scheme is a run that can proceed; one that exposes a gap between the drawing and the process is a gap discovered at the cheapest possible moment. The tolerance and finish scheme that is written feature by feature, measured instrument by instrument, and verified at the first article is the scheme that survives production, and that is the entire purpose of specifying it in the first place.
The buyer's rule of thumb: assign the band to the feature that needs it, name the datum it is measured from, call the finish where it functions, and require the measurement evidence in the RFQ. The numbers you specify are the numbers you receive only when the scheme says exactly what they mean.
Frequently Asked Questions
What does a tolerance on a custom part really commit the shop to?
It commits the shop to a process and a measurement. A tight band means controlled machining and inspection on that feature; a loose band means standard practice. Every tight callout adds cost and time, so the discipline is to tighten only what function needs and leave the rest on a stated general class.
Why is a single blanket tolerance a bad idea?
Because it prices every feature as if it were critical. A drawing with ±0.003 mm on everything pays precision pricing on clearance holes and cosmetic faces that do not need it, and it multiplies the inspection effort. Assigning tolerances feature by feature spends the precision budget where the assembly actually needs it.
Which features deserve the tight band on a custom part?
The features that engage another part: locating bores, bearing seats, mating faces, journal diameters, and any surface that positions or seals. Clearance holes, structural webs, and cosmetic faces do not. Test each tight callout with one question — what fails if this relaxes to the next band?, and let the answer decide.
What does a surface finish number mean in practice?
Ra is the arithmetic average of the surface profile, and each value tracks a process. The as-machined default is around Ra 3.2 µm; Ra 1.6 µm needs fine machining; Ra 0.8 µm means a grinding pass or a slow finish cut; finer values need grinding, lapping, or polishing. Each step down adds an operation, so the finish should be called only where it functions.
How do coatings and treatments change what I measure?
Anodizing and plating grow the surface, and heat treatment can move geometry, so the drawing should state what is measured after the treatment and what allowance was machined before it. A part machined to final size before anodizing can come out oversized; a sealing surface should state whether the finish applies to the base metal or the coated surface.
Which measurement evidence should accompany a tolerance callout?
The instrument for each critical feature and the result against the tolerance. A CMM reads a bore, a gauge reads a thread, a roughness tester reads the finish, and the report should name which was used for which value. Measurement without a named instrument is a number without a method, and a method is what makes the number evidence.
How do I write the RFQ so I receive the numbers I specify?
State the tolerance per feature or state the general class for the rest, name the finish with its process expectation, and list the measurements the report must contain. Ask the supplier to confirm per feature what it will hold and how it will measure. A reply that names the process and the proof is quoting the part you drew; one that only repeats the numbers is not.
Need your tolerance scheme reviewed feature by feature?
Send the drawing through the contact page — the review returns the per-feature bands, the datum scheme, and the finish plan with their cost effect, in writing.