
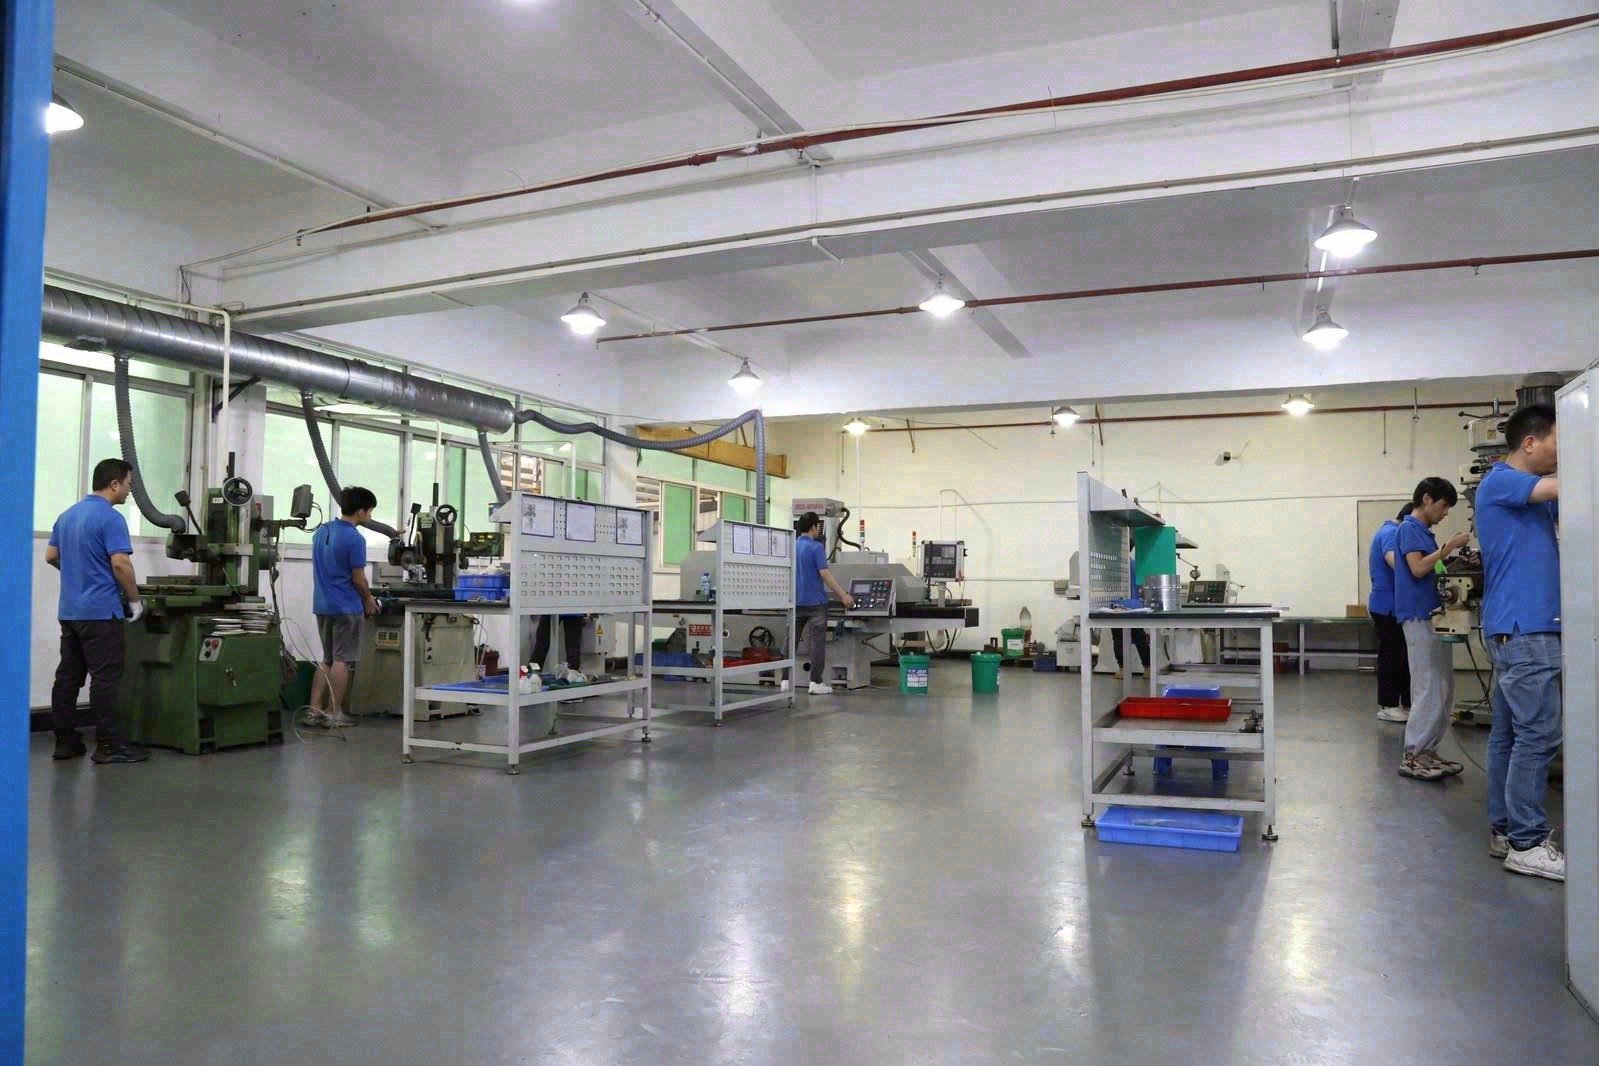
Every buyer wants a number, and the honest answer is that a custom machined part does not have one price — it has a price at a quantity. The material, the machining time, the finishing, and the inspection set the base, and the batch decides how the fixed costs of programming and setup spread across it. China changes the rates beneath those lines, but it does not change the shape of the cost. This guide walks a buyer through what a quote actually prices, which levers move it most, how traceability and documentation sit in the number, and how to compare quotes fairly at the quantity you really need.
What does a custom machined part quote actually price?
A quote prices the same layers for every custom part. Material is bought in its form and size, and you pay for the whole stock even when much of it becomes chips. Machining is machine time — the hours the part occupies the spindle, priced by the class of machine and the operations the geometry demands. Finishing and heat treatment are process steps with their own minimums. Inspection is the metrology that proves the tolerance claims. And the setup — programming, fixturing, and preparation — is the fixed cost that the batch spreads.
Read your next quote against that list. A transparent quote shows each element and lets you question it by name; a lump sum hides the same information inside a number you cannot take apart. The value of the itemized quote is the negotiation it enables: when you can see that finishing is a third of the price, you can ask whether the finish is necessary, and when you can see that setup dominates a short run, you can see why the larger batch price per unit is far lower. The layers are the levers, and the itemized quote is what makes them visible.
Which cost drivers move a custom part quote most?
Geometry and material usually set the base, and tolerance, finishing, and quantity move it from there. A complex geometry with many operations carries the most machine time, because each operation is a setup, a run, and an inspection point. Material sets the stock price and the cycle time, from aluminum at the economical end to titanium and the nickel alloys at the expensive end. The table below ranks the levers by how much they typically move a quote.
| Cost driver | What it costs | How to control it |
|---|---|---|
| Geometry and operations | Machine time across setups and tools | Reduce features the design does not need |
| Material | Stock price plus cycle-time effect | Specify the right grade; match the stock to the envelope |
| Quantity | How setup and fixed costs spread | Quote two quantities and read the amortization |
| Finishing and heat treatment | Process steps with minimum batch costs | Match the finish to the part's actual requirement |
| Tolerance and inspection | Slower passes, metrology, scrap risk | Spend the tight band on the features that control function |
The pattern to notice is that the biggest levers live inside the drawing. A feature the design does not need is pure cost; a tolerance that does not control function is pure cost; an operation that a small change eliminates is pure savings. The cheapest way to lower a custom part quote is usually not to find a cheaper supplier but to find a cheaper specification, which is exactly what a design-for-manufacturing review exists to surface before the price is committed.
How does quantity reshape the per-part price?
Quantity is the most visible lever because it bends the unit price steeply. The fixed costs — programming, fixturing, and setup — do not change whether you order one part or five hundred; they spread. At five pieces the setup dominates the unit price, at fifty it is a noticeable share, and at five hundred it rounds to a fraction of the machining line. This is why the unit-cost curve falls fast at first and flattens as volume grows, and why quoting a single quantity never tells you what the part really costs.
The practical move is to quote two quantities at once — the batch you need now and the repeat batch you may order later — and read the gap between the two unit prices. The gap is the amortization curve, and it tells you how cheaply scale buys itself. It also exposes the common mistake of buying a large batch to chase a low unit price when real demand is small, which ties cash to inventory the saving does not justify. The economical quantity is the one that meets your real demand at the lowest total cost, not the one that makes the unit number look best on paper.
How does material choice sit in the price of a custom part?
Material moves the quote on two lines: the stock price and the cycle time. Aluminum is the baseline on both — inexpensive stock that cuts fast — which is why it dominates custom parts that do not need more. Steel and stainless step up in stock and slow the cutting, with the free-machining grades at the low end and the tougher corrosion grades higher. Titanium and the nickel alloys sit at the top of both levers, and their true cost is easy to underestimate because the material bill is obvious while the slow cycle and tool wear only appear when the machine runs.
Material is not a place to save money by substitution. A part that needs 316L is not served by 304, and a structural part designed for 7075 is not represented by 6061; the money saved on the wrong grade is lost on the first failed part. Material is a place to save money by discipline — buy the stock size that matches the envelope, specify the grade that matches the function, and let the supplier flag when the drawing calls an expensive grade for a feature that does not need it. The supplier that questions your material is saving you money; the one that quotes whatever you wrote is billing you for it.
How much do tolerance and inspection add to a custom part?
Tolerance is where quotes climb fastest, because each step tighter multiplies cost across machine time, tooling, and metrology at once. A general tolerance runs on normal feeds with a standard inspection pass. A critical feature at ±0.003 mm needs finishing passes and a CMM measurement with a recorded value; a feature beyond the machining band needs a grinding operation at ±0.002 mm — a different machine class and a different price. The bands are fixed, and the drawing should spend them only where function demands.
The inspection budget follows the same logic. Every critical callout is a measurement and a line on the report, and the metrology time is real. A drawing with a short list of key characteristics inspects quickly and quotes cleanly; one that holds everything at the tight band inspects slowly and prices the worst case. When the DFM review asks whether a tolerance is necessary, it is really asking whether you want to pay the tight-band premium on that feature, and on a custom part, the honest answer is usually no, because the band belongs on the features that mate, seal, or carry the load.
What does finishing and heat treatment add, and where does traceability sit?
Finishing carries costs that do not scale with part count. Anodizing a small order still pays for the rack and the run; plating pays for the line setup; heat treatment pays for the cycle and its certificate. On a low-volume custom part the finishing line can rival the machining line, which makes the finish specification a real cost decision. Match the finish to what the part must do — a functional part that will be tested and revised does not need the cosmetic anodize class of a customer demo — and name it at quoting so the price does not reopen later.
Traceability and documentation sit in the quote as a small overhead when they are built in. A shop that records the material lot, the process, and the measured values as the work runs prices the record as part of the process; one that would assemble it after the fact prices a rebuild. The same record that supports a recall or an audit is the record that makes a quote honest, because the measured values are the evidence behind the tolerance claim. When you compare quotes, ask how the record is produced and what it contains — the difference between a process that records and a process that reconstructs shows up in the price and in the audit alike.
One-time items belong on the table as well. A custom part may carry programming, a special fixture, or a dedicated tool that is quoted once regardless of quantity, and a transparent quote shows these as one-time lines rather than folding them into the unit price. When the quantity is small, the one-time share is significant and worth questioning — a fixture the supplier already owns for a similar part should not be re-quoted as new. Ask what is one-time and what is per-part, because the split decides how the price behaves when the quantity changes, and it is the difference between a quote you can scale and one you must re-negotiate at every order. Read the split before you order, and the unit price will not surprise you when the volume arrives.
How do you compare custom machining quotes from China fairly?
Comparability starts with the input. Send the identical specification to every candidate — the model and the drawing at a named revision, the material with its condition, the tolerance callouts, the finish by class, and the quantity — and require the same quote structure with material, machining, finishing, inspection, and freight on separate lines. Compare the total delivered cost at your real quantity, not the unit price in isolation, because freight and duties belong in the comparison and a quote that hides them is incomplete.
When the quotes diverge, read the spread as information. A wide spread means someone has read the drawing differently — a different setup count, a different reading of the tolerance note, a finish assumed in-house by one supplier and quoted at a processor by another. Chase the outlier with questions before you chase it with an order, and the answer usually exposes a specification gap you are glad to find at quoting rather than at the first article. A quote that itemizes and explains the cost drivers is one you can hold to; a lump sum is a number you cannot question until it arrives.
How do you control total cost across a custom part program?
Total cost is more than the unit price multiplied by quantity. Add the freight and duties to get the landed cost, and add the softer costs: the engineering time on the drawings, the receiving inspection, the inventory the transit forces, and the cost of a revision that arrives late. A supplier that quotes slightly higher but ships a clean first article with paperwork that matches can be cheaper than one that wins the unit number and costs a week of reconciliation on every lot. The controls are structural: itemize the quote, lock the documentation list, and confirm the specification in writing so the invoice cannot grow with unagreed extras.
Then manage the program in stages priced at their own quantities. Validate the design on a single part while it is unproven, move to a small batch once the drawing is stable, and scale at the quantity your demand supports with the first-article package as the baseline every repeat lot is measured against. The parts guide on this site shows how material, tolerance, and finish land on a quoted custom part, and the traceability FAQ covers how the record behind the part is produced and what it contains.
Frequently Asked Questions
What does a custom machined part from China cost?
There is no useful single price — the number is set by the part and the quantity. A quote prices material, machining, finishing, and inspection, shaped by the batch that spreads the setup. The reliable benchmark is to quote the identical specification from three suppliers and compare their structures.
Why does a small quantity cost so much more per part?
Because the fixed costs — programming, fixturing, and setup — spread across the batch. At low quantity the setup dominates the unit price; at volume it rounds to almost nothing. Quote two quantities and the gap between them shows how cheaply a larger order can run.
Which cost drivers move a custom part quote most?
Geometry and material usually set the base; tolerance, finishing, and quantity move it from there. A complex geometry carries the most machine time, a tight tolerance adds metrology, and finishing carries minimum batch costs. The drawing is where most of the cost is decided.
Does traceability add to the price of a custom part?
Traceability is cheap when built into the process and expensive when bolted on afterward. A shop that records the chain as it runs prices it as a small overhead; one that would reconstruct records prices a rebuild. Ask how the record is produced before assuming the cost.
How much does a tighter tolerance add to a custom machined part?
Every step tighter multiplies cost across feeds, finishing passes, metrology, and scrap risk. Machining holds fit and alignment features to ±0.003 mm, with Cpk of 1.67 or higher, and grinding reaches ±0.002 mm. Those bands belong on the features that control function.
How do I compare custom machining quotes from China fairly?
Send the identical specification and require the same quote structure, with material, machining, finishing, inspection, and freight on separate lines. Compare total delivered cost at your real quantity. A quote that itemizes and flags the cost drivers is comparable; a lump sum is not.
What drives a quote up after the first email?
Incomplete specifications. A material condition not named, a finish without a class, a tolerance left to a default — each gap forces the supplier to assume, and assumptions land on the conservative side. Complete the drawing and the requirement list before quoting, and the number stops moving.
Have a custom part you want priced with the cost drivers shown?
Email [email protected] or call +86 13126536955 for a DFM review and an itemized quote that shows where the cost sits and what you can relax.